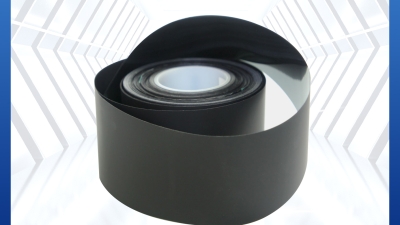
You know, in today’s fast-moving tech world, Electronic Insulation Film has really become a must-have across so many industries. It’s basically the shield that helps protect sensitive electronic parts from stuff like moisture, dust, and temperature changes—that kind of thing. I recently came across a report from MarketsandMarkets that says the global market for these materials might hit around USD 37.4 billion by 2025, growing at roughly 6% every year. Not too shabby, right? But it’s not all smooth sailing—manufacturers still face some pretty serious challenges, like making these films better at handling heat, lasting longer, and being more eco-friendly.
That’s where companies like Dongguan New Youwei Adhesive Products come in. They’re really pushing the envelope with innovative optical protective films and have earned a solid reputation—working closely with industry giants like Foxconn, Samsung, and LG. It’s clear they’re totally committed to developing top-notch products and helping upgrade how we use Electronic Insulation Film in today’s tech manufacturing. Pretty exciting stuff, if you ask me.
Challenges in Material Selection: Comparing Polyimide vs. Polyester in Electronic Insulation Films
Picking the right materials for electronic insulation films isn't exactly a walk in the park, especially when you’re comparing the two big players: polyimide and polyester.  Polyimide films are kind of the rock stars here — they’re known for handling crazy high temperatures and keeping electrical stuff insulated like pros. That makes them perfect for tough environments, think aerospace or really advanced electronics. The catch? They tend to be more expensive to produce, which can be a real dealbreaker for companies trying to keep costs down.
Now, polyester films are like the budget-friendly alternative. They won’t give you the same thermal resilience, but they do the job pretty well if temperatures and electrical stresses aren’t too extreme. The problem is, when things get truly demanding, polyester can start to struggle — it just doesn’t handle heat as well as polyimide. As industries keep pushing forward, it’s all about striking that sweet spot between performance and keeping costs manageable. Honestly, engineers have to weigh the specific needs of each project pretty carefully before they pick which material to go with.
Impact of Temperature Stability on Electronic Insulation Performance in High-tech Industries
You know, when it comes to modern high-tech industries, the stability of temperature really plays a huge role—it's honestly a game-changer for how well electronic insulation performs. Lately, there’s been some pretty exciting progress in composite materials, especially when it comes to balancing thermal insulation with strength. For example, researchers have come up with mathematical models that include thermal insulation fillers along with reinforcing fibers, and guess what? These models show pretty remarkable improvements not just in keeping heat at bay but also in making the composites more durable. That’s especially important in environments where temperatures can swing wildly, which can totally mess up electronic performance if you’re not careful.
And the market side of things? Well, it’s looking pretty bright. Experts predict that the market for top-tier insulation will jump from about 15.5 billion USD in 2025 to nearly 30 billion USD by 2035—a solid growth rate of around 6.8%. That’s mainly driven by innovations in materials like polyolefins, which are pretty key in high-voltage DC applications and help keep power transmission steady regardless of weather or temperature changes. Plus, we’re seeing cool new structures like polymer-based insulations and 'sandwich' composites, which are really pushing the envelope when it comes to maintaining electrical and thermal stability. All these advancements aren’t just about better performance—they’re also pushing us toward more sustainable solutions in the long run.
Cost Analysis: Evaluating the Economic Factors in Electronic Insulation Film Production
Manufacturing electronic insulation films is becoming more and more important in today's industries, but let’s face it, it’s not without its fair share of economic hurdles. One big thing that impacts costs is the price of raw materials. Things like polymers and additives can fluctuate quite a bit because of supply chain issues, so manufacturers are always trying to adjust their sourcing strategies on the fly. This kind of price juggling makes it pretty clear that doing thorough cost analysis is key if you want to stay competitive out there.
When it comes to cutting down costs, it’s worth thinking about adopting some of the latest tech to boost efficiency. Automating parts of the process can really help speed things up, cut down on labor expenses, and also reduce waste. Plus, recycling scrap materials or leftovers isn’t just good for the environment — it can actually save some serious money too.
Another smart move is to work with a bunch of different suppliers. That way, you get more wiggle room on prices, and it’s easier to handle sudden cost hikes or shortages. The trick is to keep reviewing and tweaking your strategies as things evolve because in the world of electronic insulation films, staying flexible is what keeps you ahead of the game.
Defining Industry Standards: A Comparison of ASTM vs. IEC Guidelines for Insulation Films
In today’s fast-changing world of modern industries, there’s been a huge spike in the demand for electronic insulation films. Because of that, having clear, standardized guidelines has become pretty crucial. Two big organizations come into play here: ASTM (American Society for Testing and Materials) and IEC (International Electrotechnical Commission). They each have their own standards for these materials. ASTM tends to focus more on how the product performs — so, they’re all about practical testing that matches real-world use. This helps manufacturers create films that can handle the actual conditions they’ll face, which is especially important for electronics where you simply can’t afford failures.
On the flip side, IEC’s standards are more about creating a globally accepted framework. They put a strong emphasis on safety and making sure things run smoothly across different regions. For companies working in international markets, IEC standards are kind of a must-have because they ensure your insulation films meet safety norms everywhere. But here’s the thing — choosing between ASTM and IEC standards can really impact how you develop your products and stay compliant with regulations. So, manufacturers need to think carefully about which standards fit best with their target markets. As new tech keeps pushing industries forward, the standards you pick will definitely play a key role in driving innovation and long-term success.
Challenges Faced with Electronic Insulation Film in Modern Industries - Defining Industry Standards: A Comparison of ASTM vs. IEC Guidelines for Insulation Films
| Aspect | ASTM Guidelines | IEC Guidelines | Common Challenges |
| Thermal Resistance | Test Method ASTM D5470 | IEC 60216 standards | Variation in thermal stability performance |
| Dielectric Strength | ASTM D149 | IEC 60243 | Inconsistency in breakdown voltage across materials |
| Chemical Resistance | ASTM D543 | IEC 60684-5 | Limited compatibility with certain solvents |
| Mechanical Properties | ASTM D638 for tensile strength | IEC 62006 | Inadequate assessment of stress-strain behavior |
| Flame Retardancy | ASTM E84 | IEC 60332 | Variability in fire behavior under different conditions |
Examining the Physical and Chemical Resistance of Various Insulation Films in Electronics
In the fast-changing world of electronics, picking the right insulation films is pretty crucial if you want your devices to last and work reliably. These films need to stand up to things like heat, moisture, and chemicals because all those environmental factors can really mess with the performance of your electronic parts. By taking a good look at the different types of insulation films out there, companies can make smarter choices to boost durability and avoid early failures.
There are a bunch of options like polyimide, polyester, and fluoropolymer films, each bringing their own strengths to the table. For instance, polyimide films are known for handling high temperatures and tough mechanical demands—perfect for high-end, demanding applications. On the flip side, fluoropolymer films are great when it comes to resisting chemicals, keeping electronic gadgets safe from all sorts of aggressive stuff. Of course, each kind has its own quirks and challenges, so it’s really important for manufacturers to understand these differences if they want to design devices that last longer and break down less in the field.
Future Trends: Emerging Technologies and Innovations in Electronic Insulation Materials
The world of electronic insulation materials is changing pretty fast these days, thanks to some really cool new technologies coming into play. One of the most exciting developments is photosensitive polyimide, or PSPI for short. It’s expected to hit a market value of around $51 billion by 2025! Everyone's talking about how lightweight and heat-resistant these materials are, which makes PSPI super important in the insulation film scene.
On top of that, the market for electronic-grade bisphenol A epoxy resin is also showing some solid growth. It’s projected to go from about $120 million in 2024 to nearly $164 million by 2032. That steady climb just shows how much folks are investing in materials that can do better in electronic use. And let's not forget the cable materials — like copper and polymer insulations — which are set to really take off thanks to new tech and the boom in telecom and consumer gadgets.
Here at Dongguan New Youwei Adhesive Products Co., Ltd., we’re constantly pushing the boundaries with our optical protective films. We’re committed to quality, and that’s why we’re proud to be a go-to supplier for some of the biggest brands out there. By focusing on these emerging materials, we’re not just staying ahead — we’re helping build a smarter, more sustainable future for electronic insulation all around.
Maximizing Energy Efficiency: The Cutting-Edge Benefits of Aerogel Ultra-Thin Heat Insulation Film
The emergence of aerogel ultra-thin thermal insulation film marks a significant milestone in enhancing energy efficiency, especially in sectors where space is a premium. This cutting-edge material boasts an impressive low thermal conductivity of around 0.013 W/m·K, making it one of the best insulating materials available today. According to a recent industry report by MarketsandMarkets, the demand for advanced thermal insulation materials in various applications, such as electronics and construction, is expected to grow at a CAGR of 8.2% from 2021 to 2026. Aerogel, with its unique properties, is poised to lead this growth trajectory.
In consumer electronics, where heat management is crucial, this ultra-thin film is engineered to optimize heat distribution while simultaneously safeguarding sensitive components. By utilizing this innovative insulation technology, manufacturers can design sleeker products without compromising on performance or safety. The flexibility of the aerogel film allows for easy integration into compact devices, enabling brands to push the boundaries of design while maintaining energy efficiency.
Moreover, the use of aerogel insulation is becoming increasingly relevant in sustainability efforts. With the construction industry responsible for nearly 40% of global energy consumption, enhancing building materials with aerogel can significantly reduce energy loss. A report from the U.S. Department of Energy highlights that implementing high-performance insulation materials like aerogel can lead to energy savings of up to 30% in buildings, reaffirming the material's pivotal role in the transition towards greener architecture.
FAQS
: Polyimide films are known for their superior thermal stability and excellent electrical insulation properties, making them highly suitable for high-temperature environments like aerospace and advanced electronics.
Polyester films are a more cost-effective alternative compared to polyimide films, offering decent insulation characteristics for applications where temperature and electrical stresses are relatively low.
Engineers must balance performance capabilities with cost-effectiveness and evaluate the specific needs of each application to make the best material choice.
ASTM focuses on performance-based testing to meet industry needs, while IEC provides a globally accepted framework emphasizing safety and interoperability across different regions.
The choice of insulation film standards can significantly impact product development and regulatory compliance, influencing market goals and ensuring safety criteria are met.
Common types of insulation films include polyimide, polyester, and fluoropolymer, each with unique properties regarding heat resistance and chemical stability.
Insulation films must demonstrate resistance to high temperatures, moisture, and exposure to chemicals to ensure the longevity and reliability of electronic components.
Fluoropolymer films excel in chemical resistance, protecting electronic devices from aggressive substances that could compromise their performance.
Understanding the distinct advantages of different insulation films allows manufacturers to optimize designs, enhancing the durability and reliability of their electronic products.
Selecting the right insulation film standards is critical for innovation and long-term success as industries integrate advanced technologies into their products.
Conclusion
The blog titled "Challenges Faced with Electronic Insulation Films in Modern Industries" really dives into some of the big issues that affect how well these insulation films work and how useful they are. It touches on things like choosing the right materials—comparing polyimide and polyester—and why temperature stability is such a big deal, especially in high-tech stuff. Plus, it looks at the economic side of things—how production costs come into play and what it means to stick to industry standards, like ASTM versus IEC guidelines. The article also reviews how resistant different insulation films are to physical wear and chemicals, giving us some good insights into which ones are best suited for specific electronic needs.
At Dongguan New Youwei Adhesive Products Co., Ltd., we're proud to be a leader in optical protective film technology. We’re always striving to tackle these challenges head-on by developing innovative electronic insulation films that can handle the tough demands of major players like Foxconn and Samsung. Staying ahead of the latest trends and tech keeps us motivated, and our goal is to deliver products that don’t just meet expectations but actually go beyond them. We genuinely care about helping our customers find the perfect solutions for their needs.